Every wire EDM request complete per part.
Blake reads contour tolerance, roughness and material from the drawing and puts them beside the model as proposals, part by part.
Everything on the table before you price.
- SDX-EDM-012_Rev-B.pdf
- SDX-EDM-012_Rev-B.step
Read from the drawingTo check
- Material
- 1.2379
- Hardness
- 60–62 HRC, supplied hardened
- Contour tolerance
- ±0.005 mm
- Contour roughness
- Ra 0.4
Complete part by part.
Model and drawing
Paired by file name. Any doubt stays a question for you.
Requirements
Tolerance, roughness and material from the drawing, ready to confirm.
Revisions
Every revision kept, with its own files.
- Part
- 160 × 110 × 32 mm
- Envelope
- 550 × 350 × 400 mm
- Axes and reach
- X, Y and Z, with U and V for taper cutting
ManufacturabilityUnder review±0.005 mm and Ra 0.4 in the contour, to confirm
Hourly rateYour rate for this machine
- 1Flaton the table, aligned to the reference edge
- Wiretype and diameter set by your specialist
- Start holes Ø1.5one per inner contour
Recorded with travels and rate.
Envelope and axes
Recorded per machine.
Hourly rate
Your rate, per machine.
One machine park
Wire EDM machines beside your mills and lathes.
Where wire EDM time goes.
Skim cuts.
A tighter tolerance and a lower Ra mean more skim cuts, depending on height and material.
Wire and start hole.
A narrow slot needs a thinner wire, and every inner contour its own start hole.
A missed contour.
On a slow process, one missed contour can cost hours of machine time.
The next cost model on the same requirements and machines.
Underneath Blake sits Subduxion’s manufacturing world model: how a part, its requirements, your machines and your team’s decisions fit together. The cost model for this process is built on the same requirements and machines.
- Model, drawing and requirements are already in place, part by part.
- Next: time and price for this process from the same requirements, on your own machines.
- The machined parts in the same request are already estimated.
Frequently asked questions
Does Blake estimate wire EDM work?
Blake gets every wire EDM request ready for your estimate: model and drawing per part, tolerance, roughness and material as proposals, and your wire EDM machines with envelope and rate. Next comes the estimate: wire, skim cuts and cutting time from contour, height and material.
How do I avoid overlooking a requirement?
Blake places the drawing requirements as proposals beside the model, part by part, so you confirm or correct them one at a time. Who changed what, and when, stays visible to your colleagues.
Does Blake handle hardened or pre-machined supplied parts?
Yes. The customer’s model and drawing go into the request per part, with their revision, also when the part arrives milled, turned or hardened. The drawing’s requirements sit as proposals beside the model.
Which wire EDM machines can I record in Blake?
Any wire EDM machine. You record your wire EDM machines with their travels and your own hourly rate, beside your milling and turning machines.
Which files does Blake need for a wire EDM request?
A STEP model and a PDF drawing per part. Blake pairs them by file name; when a pairing is not certain, it stays a question for you instead of a silent choice.
Printing or machining: when to choose which
Category: Know-how7 min read
Design for cost: what a tolerance really costs
Category: Know-how7 min read
What a 0.02 position tolerance does to the route
Category: Know-how9 min read
Your wire EDM experience.
In every request.
In a demo, see a die plate with three inner contours made ready for your estimate.
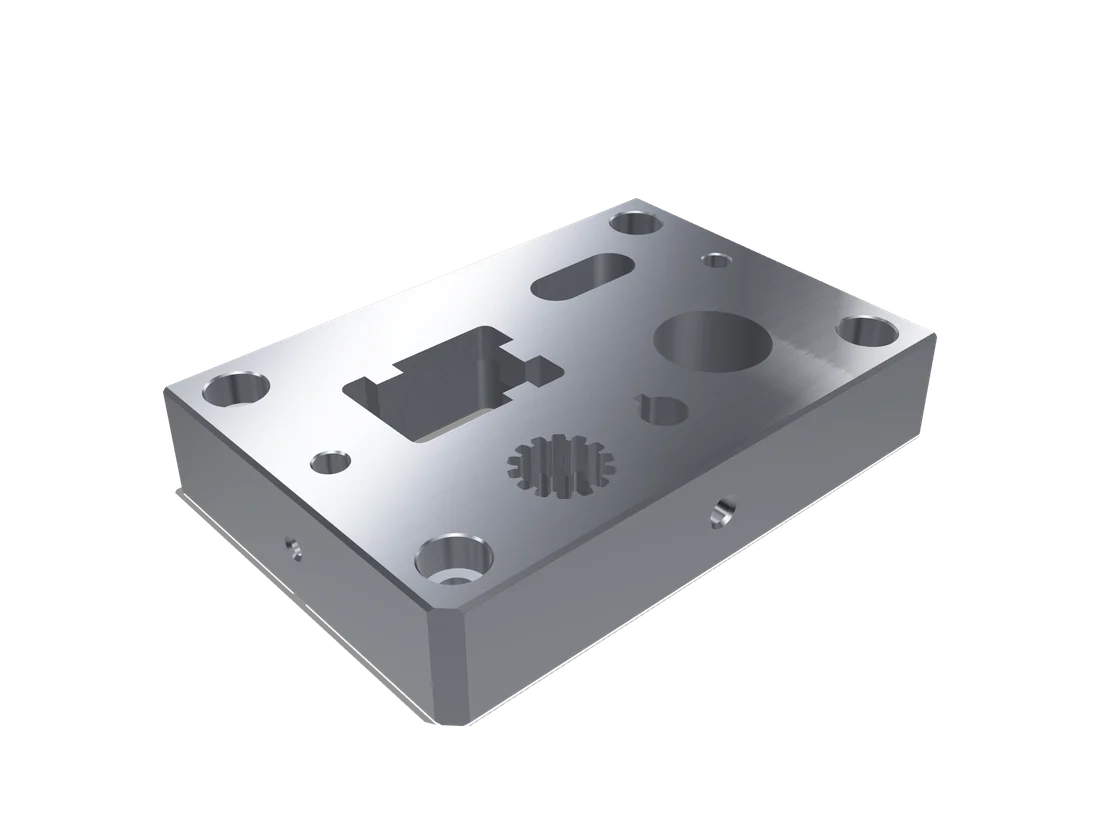
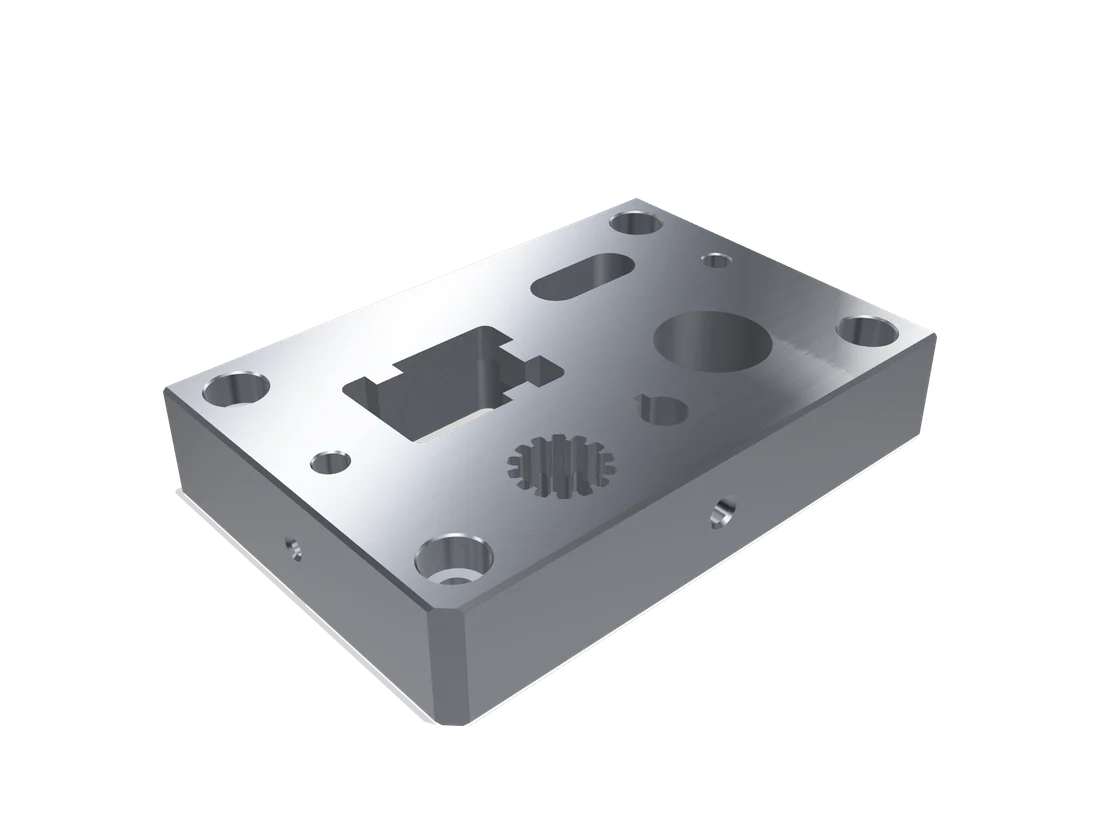
SDX-EDM-012 Rev B